1-Piperidinecarboxaldehyde → 6-Chloropyridine-3-carbaldehyde
Reaction equation

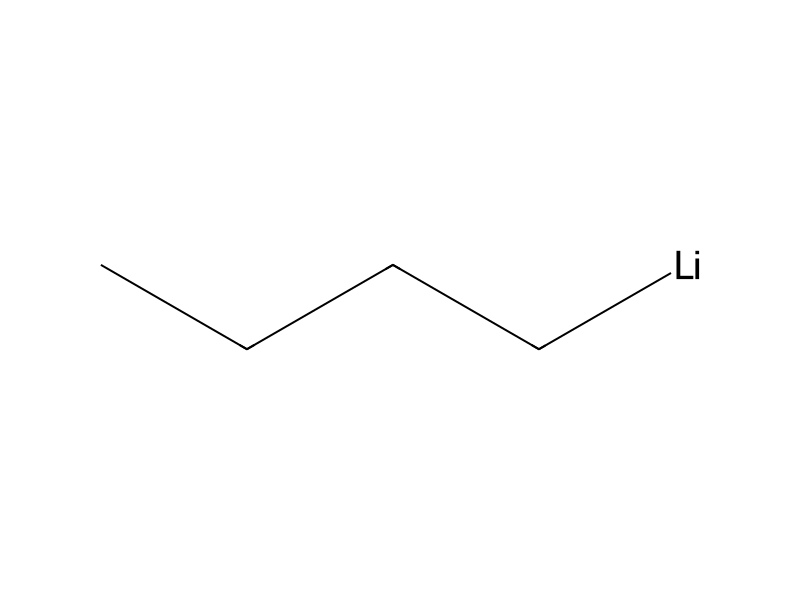
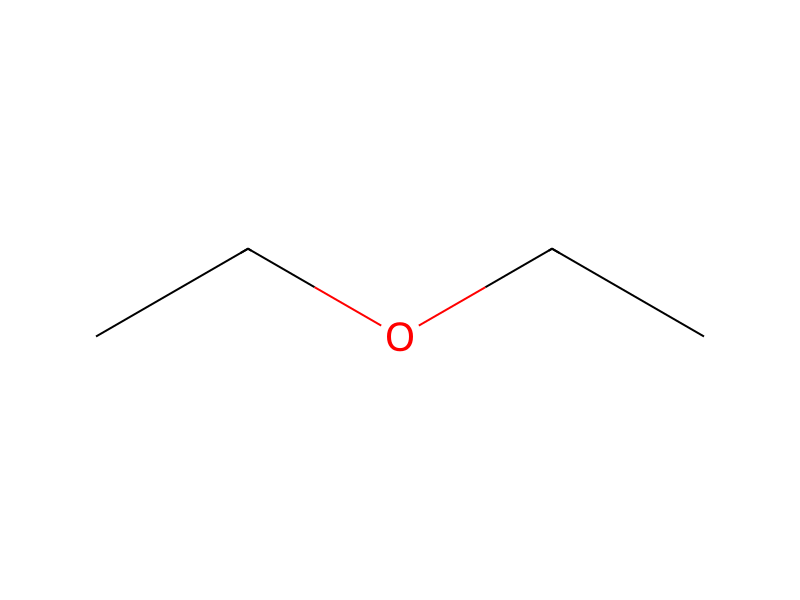
Br[C:2]1[CH:3]=[CH:4][C:5]([Cl:8])=[N:6][CH:7]=1.C([Li])CCC.[CH:14](N1CCCCC1)=[O:15]>C(OCC)C>[Cl:8][C:5]1[CH:4]=[CH:3][C:2]([CH:14]=[O:15])=[CH:7][N:6]=1Participants
Reactant 3


Product 1

Reagents, catalysts & solvents 1
Conditions
- Temperature
- -50 °C
Procedure
5-Bromo-2-chloropyridine (T-9) (15.0 g) and diethyl ether (450 ml) were put in a reaction vessel and cooled to −50° C. under an atmosphere of nitrogen. n-Butyllithium (1.57 M in n-hexane; 54.6 ml) was added dropwise in the temperature range of −50° C. to −45° C., and the stirring was continued for another 90 minutes. After the reaction vessel had been cooled to −70° C., formylpiperidine (9.70 g) was added dropwise in the temperature range of −70° C. to −65° C., and the stirring was continued for another 60 minutes while the mixture was allowed to return to room temperature. The resulting reaction mixture was poured into ice-water (500 ml) and mixed with it. Diethyl ether (200 ml) was added to the solution to separate organic and aqueous phases, and extraction was carried out. The combined organic phase was washed with water and dried over anhydrous magnesium sulfate. The resulting solution was concentrated under reduced pressure and the residue was purified with a fractional operation by means of column chromatography (silica gel; toluene). The product was further purified by recrystallization from heptane. The solvent was distilled off and the product was dried, giving 2-chloro-5-formylpyridine (T-10) (7.01 g). The yield based on the compound (T-9) was 68%.
Workup
- temperatureAfter the reaction vessel had been cooled to −70° C.
- waitthe stirring was continued for another 60 minutes while the mixture
- customto return to room temperature
- customThe resulting reaction mixture
- additionmixed with it
- customto separate organic
- extractionaqueous phases, and extraction
- washThe combined organic phase was washed with water
- dry with materialdried over anhydrous magnesium sulfate
- concentrationThe resulting solution was concentrated under reduced pressure
- customthe residue was purified with a fractional operation by means of column chromatography (silica gel; toluene)
- customThe product was further purified by recrystallization from heptane
- distillationThe solvent was distilled off
- customthe product was dried
Sources & evidence
- ORD record
- ord-317fceed687f49219a9254e50aa28f15
- Source dataset
- uspto-grants-2013_07
- Patent number
- US08475888B2
Reaction notes
Loading…