Potassium Carbonate → Propyl 2-(2-methoxyphenyl)-3-phenyl-2-[(1,2,4-triazol-1-yl)methyl]-propionate
Reaction equation

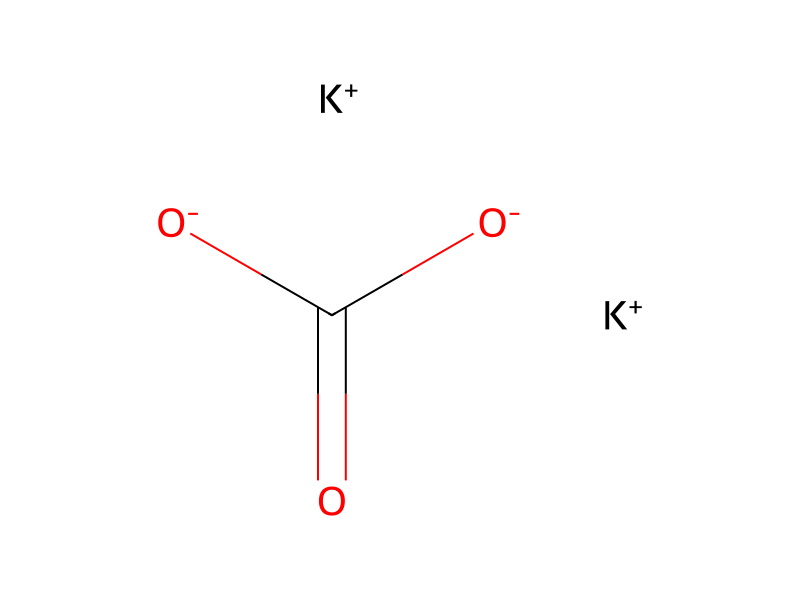
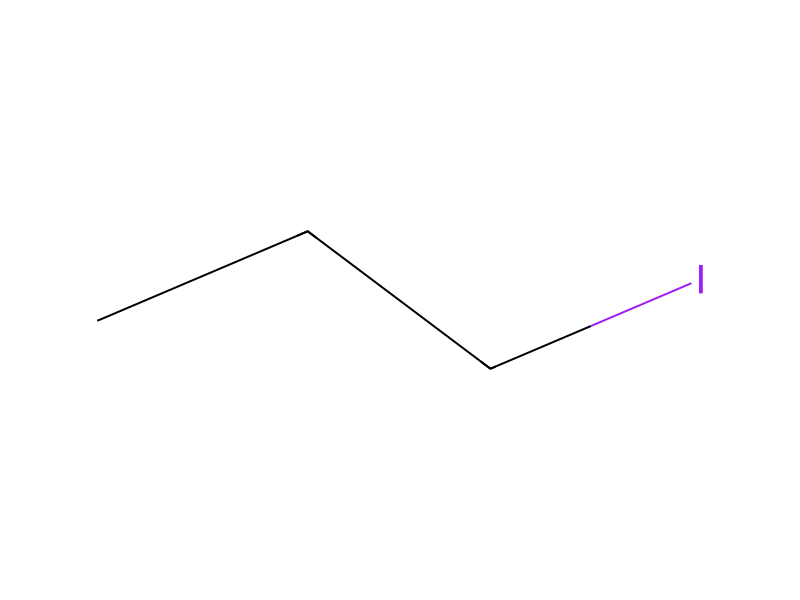
[CH3:1][O:2][C:3]1[CH:8]=[CH:7][CH:6]=[CH:5][C:4]=1[C:9]([CH2:20][N:21]1[CH:25]=[N:24][CH:23]=[N:22]1)([CH2:13][C:14]1[CH:19]=[CH:18][CH:17]=[CH:16][CH:15]=1)[C:10]([OH:12])=[O:11].C(=O)([O-])[O-].[K+].[K+].I[CH2:33][CH2:34][CH3:35]>C(C(C)=O)C>[CH3:1][O:2][C:3]1[CH:8]=[CH:7][CH:6]=[CH:5][C:4]=1[C:9]([CH2:20][N:21]1[CH:25]=[N:24][CH:23]=[N:22]1)([CH2:13][C:14]1[CH:15]=[CH:16][CH:17]=[CH:18][CH:19]=1)[C:10]([O:12][CH2:33][CH2:34][CH3:35])=[O:11]Participants
5
Reactant 3

Product 1

Reagents, catalysts & solvents 1

Procedure
A mixture of 2-(2-methoxyphenyl)-3-phenyl-2-[(1,2,4-triazol-1-yl)methyl]propanoic acid (6.0 g, 0.0178 mole) and potassium carbonate (3.6 g, 0.0213 mole) in methyl ethyl ketone (50 mL) was stirred and heated to reflux for 1 hour. Iodopropane (3.6 g, 0.0213 mole) was added and the mixture continued heating at reflux for an additional 4 hours and then allowed to cool to room temperature. The solvent was removed by distillation and 100 mL of water and 100 mL of ethyl acetate added. The organic phase was then separated, dried and concentrated on a rotary evaporator to afford 5.5 g of solid product (melting point 129°-130° C.; yield 82% ), Example 100 of Table 1.
Workup
- temperatureheated
- temperatureto reflux for 1 hour
- temperaturethe mixture continued heating
- temperatureat reflux for an additional 4 hours
- customThe solvent was removed by distillation and 100 mL of water and 100 mL of ethyl acetate
- additionadded
- customThe organic phase was then separated
- customdried
- concentrationconcentrated on a rotary evaporator
Sources & evidence
- ORD record
- ord-2b11250b70fd48e89d64a5e519f9a324
- Source dataset
- uspto-grants-1995_03
- Patent number
- US05397768
Reaction notes
Loading…