Reaction equation

[C:1]([O:6][CH3:7])(=[O:5])[C:2]([CH3:4])=[CH2:3].C([Sn](Cl)(Cl)Cl)[CH2:9][CH2:10][CH3:11].C[O-].[Na+].[CH3:19][O:20][C:21]1C=CC(O)=CC=1.C1(C=CC(O)=CC=1)[OH:29]>CCCCCCC.C(O)CO>[C:1]([O:6][CH2:7][CH2:19][O:20][C:21](=[O:29])[C:10]([CH3:9])=[CH2:11])(=[O:5])[C:2]([CH3:4])=[CH2:3]Participants




Procedure
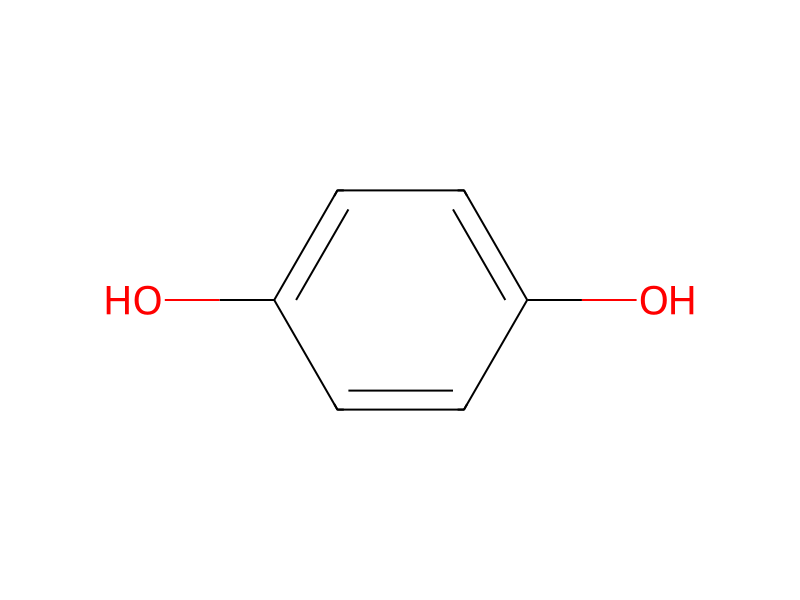
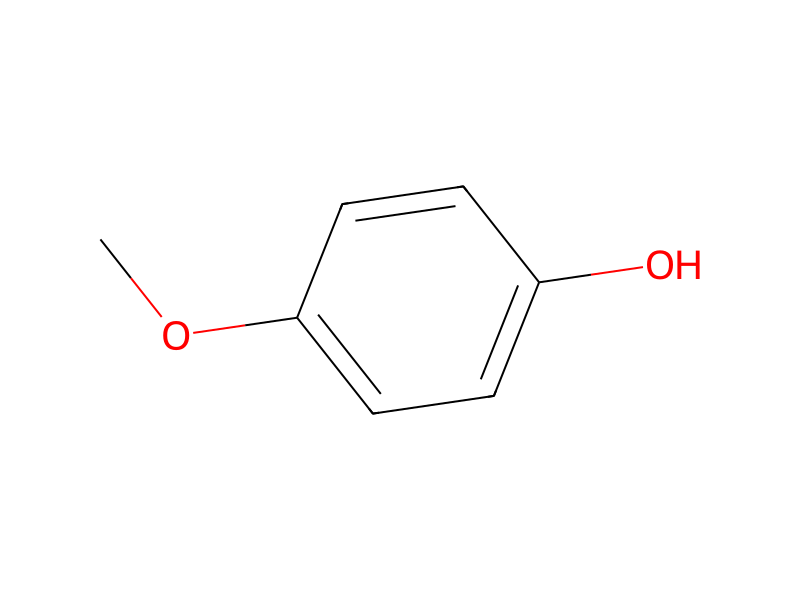
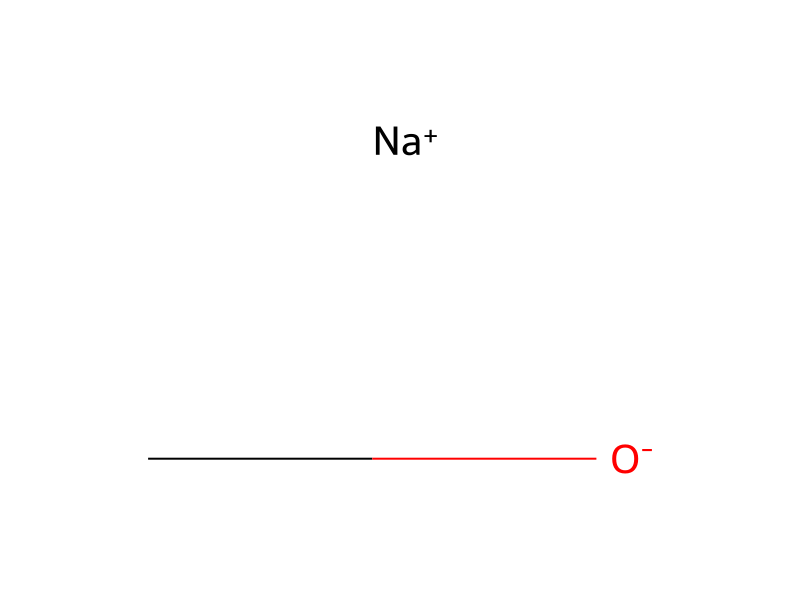
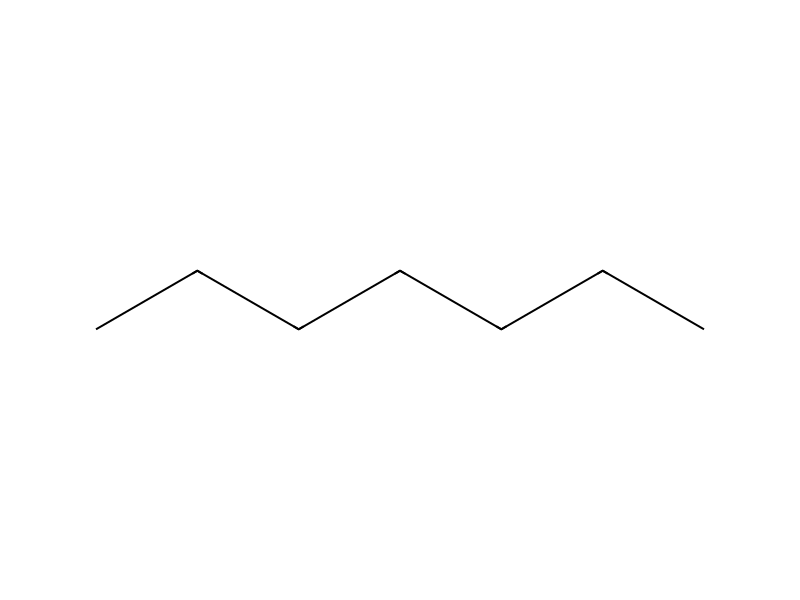
A mixture of ethylene glycol (62.0 parts), methyl methacrylate (300 parts), heptane (50 parts), butyltin trichloride (7.0 parts), sodium methoxide (5.4 parts, 25% in methanol), 4-methoxyphenol (0.5 parts) and hydroquinone (0.5 parts) was heated as in Example 1. Methanol, heptane, and excess methyl methacrylate were removed from the crude product. To remove the tin catalyst and polymerization inhibitors, the crude product containing approximately 50% solvent was washed twice with 15% sodium hydroxide at 20% of batch weight. After reducing alkalinity by washing the product with a 15% sodium chloride brine solution, the organic layer was concentrated to yield 185 parts (93% yield based on ethylene glycol) of ethylene glycol dimethacrylate (EGDMA). The purity of the final product was greater than 98%. Analysis for residual tin was 160 ppm.
Workup
- temperaturewas heated as in Example 1
- customMethanol, heptane, and excess methyl methacrylate were removed from the crude product
- customTo remove
- customthe tin catalyst and polymerization inhibitors
- washwas washed twice with 15% sodium hydroxide at 20% of batch weight
- washby washing the product with a 15% sodium chloride brine solution
- concentrationthe organic layer was concentrated
Sources & evidence
- ORD record
- ord-c699d8b312b64b27b6ebbad83ba81f1e
- Source dataset
- uspto-grants-1997_02
- Patent number
- US05606103
Linked notes
Loading…