Nitrogen → methyl 3-[5-(2-tert-butylsilyloxypropan-2-yl)-1-[(2-methylpropan-2-yl)oxycarbonyl]indol-2-yl]-1H-thieno[3,2-c]pyrazole-5-carboxylate
Reaction equation

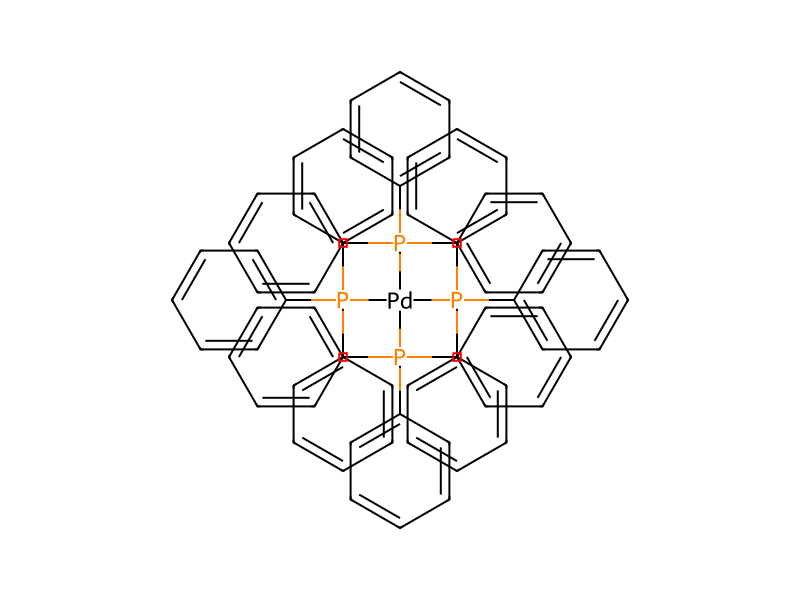
[CH3:1][O:2][C:3]([C:5]1[S:12][C:11]2[C:10](I)=[N:9][NH:8][C:7]=2[CH:6]=1)=[O:4].C(=O)([O-])[O-].[K+].[K+].[C:20]([O:24][C:25]([N:27]1[C:35]2[C:30](=[CH:31][C:32]([C:36]([CH3:44])([CH3:43])[O:37][SiH2:38][C:39]([CH3:42])([CH3:41])[CH3:40])=[CH:33][CH:34]=2)[CH:29]=[C:28]1C1C2SC=CC=2N(C(OC(C)(C)C)=O)N=1)=[O:26])([CH3:23])([CH3:22])[CH3:21].N#N>C(OCC)(=O)C.C1C=CC([P]([Pd]([P](C2C=CC=CC=2)(C2C=CC=CC=2)C2C=CC=CC=2)([P](C2C=CC=CC=2)(C2C=CC=CC=2)C2C=CC=CC=2)[P](C2C=CC=CC=2)(C2C=CC=CC=2)C2C=CC=CC=2)(C2C=CC=CC=2)C2C=CC=CC=2)=CC=1>[C:20]([O:24][C:25]([N:27]1[C:35]2[C:30](=[CH:31][C:32]([C:36]([CH3:44])([CH3:43])[O:37][SiH2:38][C:39]([CH3:42])([CH3:41])[CH3:40])=[CH:33][CH:34]=2)[CH:29]=[C:28]1[C:10]1[C:11]2[S:12][C:5]([C:3]([O:2][CH3:1])=[O:4])=[CH:6][C:7]=2[NH:8][N:9]=1)=[O:26])([CH3:23])([CH3:22])[CH3:21]Participants
Reactant 4


Product 1

Reagents, catalysts & solvents 2
Conditions
- Temperature
- 120 °C
Procedure
In two separate Smith process vials (10-20 mL capacity) are added 3-iodo-1H-thieno[3,2-c]pyrazole-5-carboxylic acid methyl ester [420 mg, 1.36 mmol, Intermediate (26)], 5-(tert-butyl-dimethyl-silanyloxymethyl)-1H-indole-2-boronic acid 1-carboxylic acid tert-butyl ester [912 mg, 2.25 mmol, Intermediate (8), prepared as described in Example 1-4 of International Patent Application Publication No. WO 02/32861], potassium carbonate (2M, aqueous, 2.25 mL) tetrakis(triphenylphosphine)palladium(0) (87 mg, 0.0752 mmol), and a mixture of toluene/ethanol (9:3 mL). The reaction tube is filled with N2 and sealed using capping device. The reaction mixture is heated to 120° C. using microwave (Personal chemistry optimizer) for 900 seconds. After reactions are over combined them into a flask, diluted with ethyl acetate (50 mL) and washed twice with water (10 mL), brine and dried over sodium sulfate. Purification by chromatography on 35 g silica gel cartridge (30-50% ethyl acetate gradient in heptane) gave two major fractions. The higher rising Rf fractions are combined and evaporated solvent in vacuo to give 5-(tert-butyl-dimethyl-silanyloxymethyl)-2-(5-methoxycarbonyl-1H-thieno[3,2-c]pyrazol-3-yl)-indole-1-carboxylic acid tert-butyl ester [653 mg, Intermediate (27)] as light yellow solid. LC/MS: 542 (M+H). The lower rising Rf fractions are combined and evaporated in vacuo to give product 3-[5-(tert-butyl-dimethyl-silanyloxymethyl)-1H-indol-2-yl]-1H-thieno[3,2-c]pyrazole-5-carboxylic acid methyl ester [253 mg, Intermediate (28)] as light yellow solid; LC/MS: 442 (M+H).
Workup
- customIn two separate Smith process vials (10-20 mL capacity)
- customsealed
- customfor 900 seconds
- washwashed twice with water (10 mL), brine
- dry with materialdried over sodium sulfate
- customPurification by chromatography on 35 g silica gel cartridge (30-50% ethyl acetate gradient in heptane)
- customgave two major fractions
- customevaporated solvent in vacuo
Sources & evidence
- ORD record
- ord-ad6569cff856468da9c4f1699aa35470
- Source dataset
- uspto-grants-2011_04
- Patent number
- US07928231B2
Reaction notes
Loading…