(3S,4S,5R)-1,3,4,5,6-pentahydroxyhexan-2-one → HCID 86703357, compound
Reaction equation

[Ca].[O:2]=[CH:3][C@@H:4]([C@H:6]([C@H:8]([C@@H:10]([CH2:12][OH:13])[OH:11])[OH:9])[OH:7])[OH:5].[OH:14][CH2:15][C:16]([C@H:18]([C@H:20]([C@@H:22]([CH2:24][OH:25])[OH:23])[OH:21])[OH:19])=[O:17].O=C[C@@H]([C@H]([C@@H]([C@@H](CO)O)O)O)O.[Cl-].[Cl-].[Ca+2]>O>[O:2]=[CH:3][C@@H:4]([C@H:6]([C@H:8]([C@@H:10]([CH2:12][OH:13])[OH:11])[OH:9])[OH:7])[OH:5].[OH:14][CH2:15][C:16]([C@H:18]([C@H:20]([C@@H:22]([CH2:24][OH:25])[OH:23])[OH:21])[OH:19])=[O:17]Participants
Reactant 5

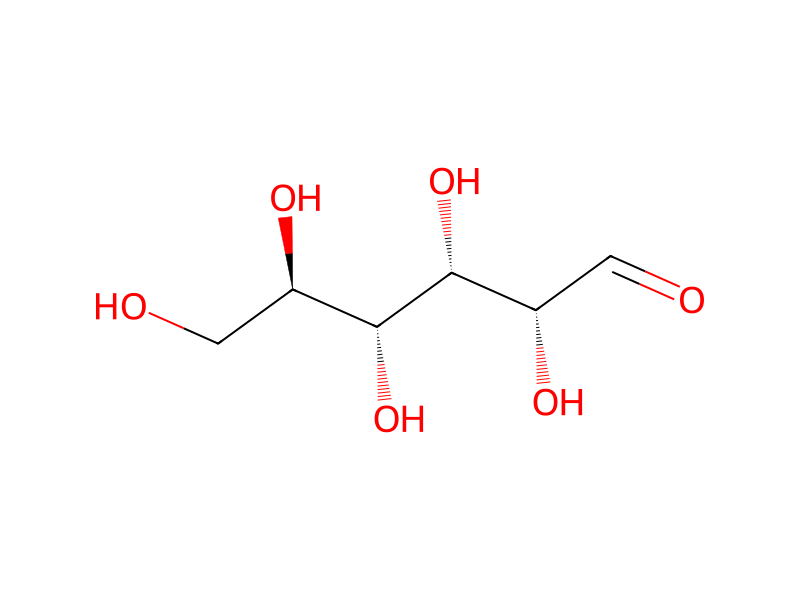
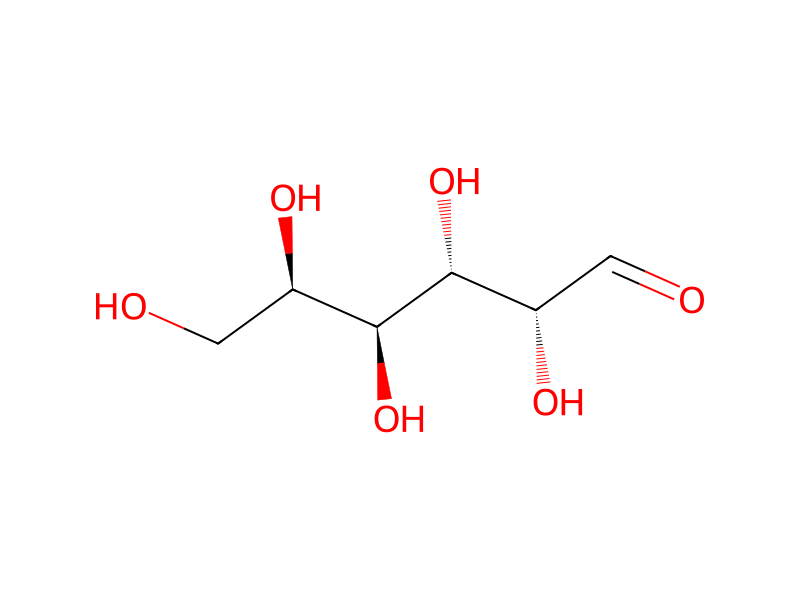

Product 1

Reagents, catalysts & solvents 1

Conditions
- Temperature
- 65 °C
Procedure
An SMB unit (available from Orochem Technologies Inc., Lombard, Ill.) was configured as a combination of 30 columns divided equally into 3 circuits. Each circuit contained 10 columns. The size of each column was 14 inch×65 inch (35.56 cm×165.1 cm) and had an empty volume of about 150 liters. Each column was packed with 117 kg of Dowex 99CA/320 resin (Available from the Dow Chemical Company, Midland, Mich.), a strong acid cation calcium exchange resin stationary phase. The 30 columns were mounted on a rotating carousal. A fluid distribution valve was located at the center of the unit. Flow rates were controlled through control panel by adjusting valves and pump rates. Each circuit was divided into 4 different zones, i.e. (2-3-2-2) configuration. (See FIG. 5) At step 1, feed in lines 830 and 831 is pumped into column 705 and Raffinate is withdrawn (faster moving components/salts) from the bottom of column 707. Desorbent in lines 800 and 810 was pumped to the top of column 701 and extract (slower moving component/sugars) was withdrawn from the bottom of column 702. A portion of the extract in lines 818 and 822 was pumped back into the column 703 and a portion of the raffinate in lines 838 and 842 was pumped to the top of column 708 to provide a Raffinate Bleed in lines 844 and 842 from the bottom of column 708. The Raffinate bleed is pumped back into column 709 to push residual desorbent out and recycle desorbent in line 805. Column 710 was stationary at any given step in order to avoid back mixing of fluids within intermediate circuits. The desorbent was RO water (reverse osmosis) at low conductivity. According to FIG. 3, the Galactose isomerate had a Brix value of 10-15 and comprised 40-60% d-tagatose, 20% d-glucose, 10-20% d-galactose and CaCl2 salts. The galactose isomerate was filtered to remove solid particulates and fed into SMB-406. The desorbent was RO water (reverse osmosis) at low conductivity. The desorbent had a pH 6.5-7.0 and was pumped at a rate of 8.5 L/min. The extract stream in line 318 was withdrawn at a rate of 2.0 L/min and the raffinate stream in line 326 was withdrawn at a rate of 8.0 L/min. A portion of the raffinate stream was pumped back into SMB as raffinate bleed at a rate of 4.5 L/min and residual desorbent was returned to the desorbent tank (Not Shown). The SMB unit was maintained at a temperature of 65° C., and the step time of the rotary valve was 1020 seconds (17 min). The SMB unit provided an extract stream comprising d-tagatose having a purity of about 95-98 wt-% of sugar at a recovery about 95 wt-% based on sugar. The raffinate stream comprised d-glucose, d-galactose and CaCl2 salts at 5-7 Brix. The raffinate stream was passed to evaporator 409 to concentrate prior to passing the evaporated raffinate/feed admixture to the ion exclusion SMB-401 for salt removal.
Workup
- customA fluid distribution valve was located at the center of the unit
- customis withdrawn (
- extractionextract (
- customwas withdrawn from the bottom of column 702
- extractionA portion of the extract in lines 818 and 822
- customto provide a Raffinate Bleed in lines 844 and 842 from the bottom of column 708
- additionto avoid back mixing of fluids within intermediate circuits
- filtrationThe galactose isomerate was filtered
- customto remove solid particulates
- customThe extract stream in line 318 was withdrawn at a rate of 2.0 L/min
- customthe raffinate stream in line 326 was withdrawn at a rate of 8.0 L/min
- custom(17 min)
- customThe SMB unit provided an extract stream
- customThe raffinate stream was passed to evaporator 409
- concentrationto concentrate
- customSMB-401 for salt removal
Sources & evidence
- ORD record
- ord-edd588ef39114048b2bc607a386d7751
- Source dataset
- uspto-grants-2014_08
- Patent number
- US08802843B2
Reaction notes
Loading…